Explore our certified, factory-direct luxury container hotel units, moveable office pods, and resort cabins designed for rapid deployment, high ROI, and zero rain leakage under typhoon conditions.
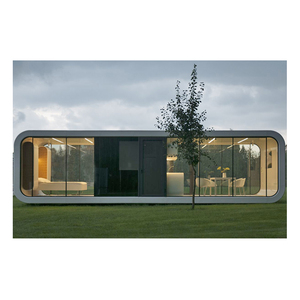
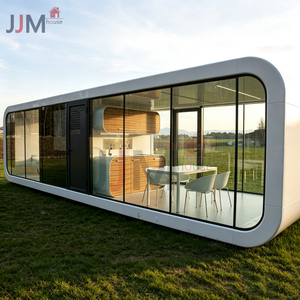
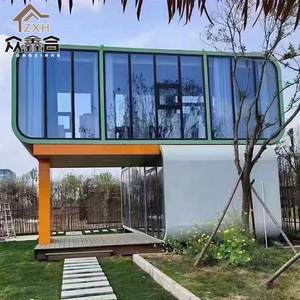
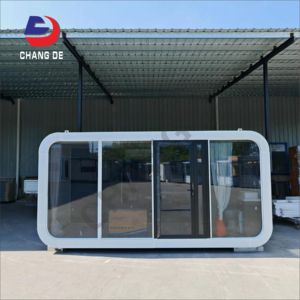
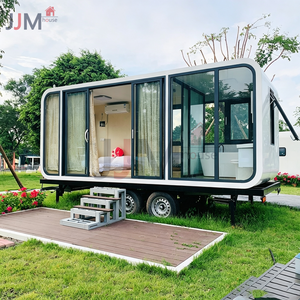
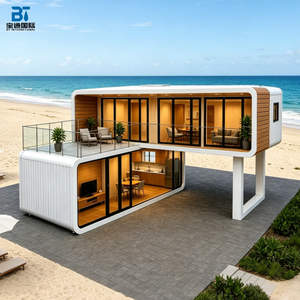
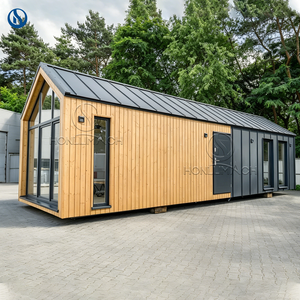
The global commercial real estate and hospitality investment landscape is undergoing a structural transition toward fast-turnaround, capital-efficient, and low-footprint building methods. As traditional brick-and-mortar construction faces skyrocketing material prices, labor shortages, and complex permitting timelines, commercial developers, eco-resort operators, and institutional procurement managers are heavily turning to prefabricated container hotels, space capsules, and luxury Apple Cabins manufactured in China.
As China’s premier container hotel supplier and exporter, our engineering ecosystem delivers fully customized, turn-key modular buildings that reduce time-to-market by up to 70%. By consolidating architectural drafting, structural steel frame fabrication, thermal barrier integration, smart MEP (Mechanical, Electrical, Plumbing) pre-fitting, and interior finishing inside automated manufacturing hubs, we eliminate weather delays and on-site trade disputes.
| Key Performance Indicator | Traditional Masonry Hotel | China Modular Container Hotel | Strategic Investment Benefit |
|---|---|---|---|
| Construction Timeline | 14 to 24 Months | 45 to 60 Days (Factory) + 7 Days (Site) | 70% Faster Yield & Revenue Realization |
| CAPEX per Key ($/m²) | $1,800 - $3,500 / m² | $450 - $950 / m² | Up to 60% Initial Capital Savings |
| Foundation Impact | Deep Concrete Piling & Excavation | Minimal Pier Points / Ground Screw Decking | Zero Ecological Damage & Simple Permitting |
| Relocation Flexibility | Fixed / Zero Mobility | 100% Relocatable / Modular Re-configuration | Asset Preservation & Residual Value |
| Acoustic & Thermal Control | Variable (Site Dependant) | STC 45+ Sound Rating / Rockwool & PU Insulation | Five-Star Guest Comfort Standard |
Professional B2B buyers must anticipate changing economic, environmental, and technological requirements when sourcing modular hospitality real estate. Over the next decade, container hotel procurement will be defined by three critical trends:
Resort developers are increasingly buying units engineered with integrated Building-Integrated Photovoltaic (BIPV) solar roofing, lithium-ion battery banks, and low-voltage DC microgrids, enabling off-grid luxury living in national parks and remote islands.
Modern buyers are ditching raw standard steel containers in favor of curved aluminum aviation alloy shells (Apple Cabins and Space Capsules) finished with PVDF fluorocarbon coatings to prevent rust under intense coastal UV and salt spray.
Turn-key container hotel units now arrive fully pre-wired with smart keyless door locks, automatic curtain tracks, integrated voice-controlled ambient lighting, and smart climate control systems linked directly to central hotel management software.
The first generation of container homes relied on modifying second-hand ISO shipping containers. While cost-effective, these legacy units suffered from condensation bridges, rigid dimensional constraints, poor ceiling heights, and high rust risk at cutouts.
Our Gen-2 Modular Engineering Platform represents a full leap forward. Instead of cutting up retired ocean freight boxes, we engineer purpose-built structural steel skeletons using Q235B/Q355B hot-dip galvanized cold-formed steel profiles combined with heavy-duty corner castings.
Constructed using 3.0mm–4.0mm heavy-duty galvanized structural steel main beams, electrostatically powder-coated for 30+ year lifespan. Tested against seismic activity up to Magnitude 8.
Wall assemblies feature 50mm–100mm high-density Polyurethane (PU) foam or Class A Non-Combustible Rockwool sandwich panels, delivering exceptional thermal conductivity as low as 0.022 W/m·K.
Eliminates external rainwater downspouts. Sloped insulated roof decks divert water into internal pillar downpipes equipped with heated anti-freezing cable channels for cold climate reliability.
Sourcing prefabricated hotel buildings from China requires complete confidence in structural compliance, factory quality assurance, and international logistics execution. Grounded in decades of industrial modular manufacturing, our operations strictly adhere to international engineering standards.
Our products hold international certifications including CE compliance for European electrical and structural safety, PCAB accreditation, D-U-N-S business registration, and PhilGEPS listing for government procurement.
Flat-pack and detachable models load up to 4 complete units per 40ft HQ container. Premium Space Capsules are shipped as complete SKD/CBU units on specialized flat-rack containers with customized export protective packaging.
Every cabin leaves the factory fully pre-plumbed and pre-wired to destination electrical standards (110V/220V, BS/EU/US/AU socket standards), complete with dry-wet separated sanitary ware, rain showers, and smart toilets.
Connect directly with our senior engineering desk to receive custom architectural drawings, stowage-optimized loading plans, and competitive factory-direct B2B quotation packages within 24 hours.
Inquire Now